- Home
- Work
Impeller machining, cast pump covers and turned appliance parts — real work from our shop
Every photo on this page is a real part milled or turned in our factory, not stock imagery. Each one states the process, the machine and how it was checked, so you can see what your part will go through.
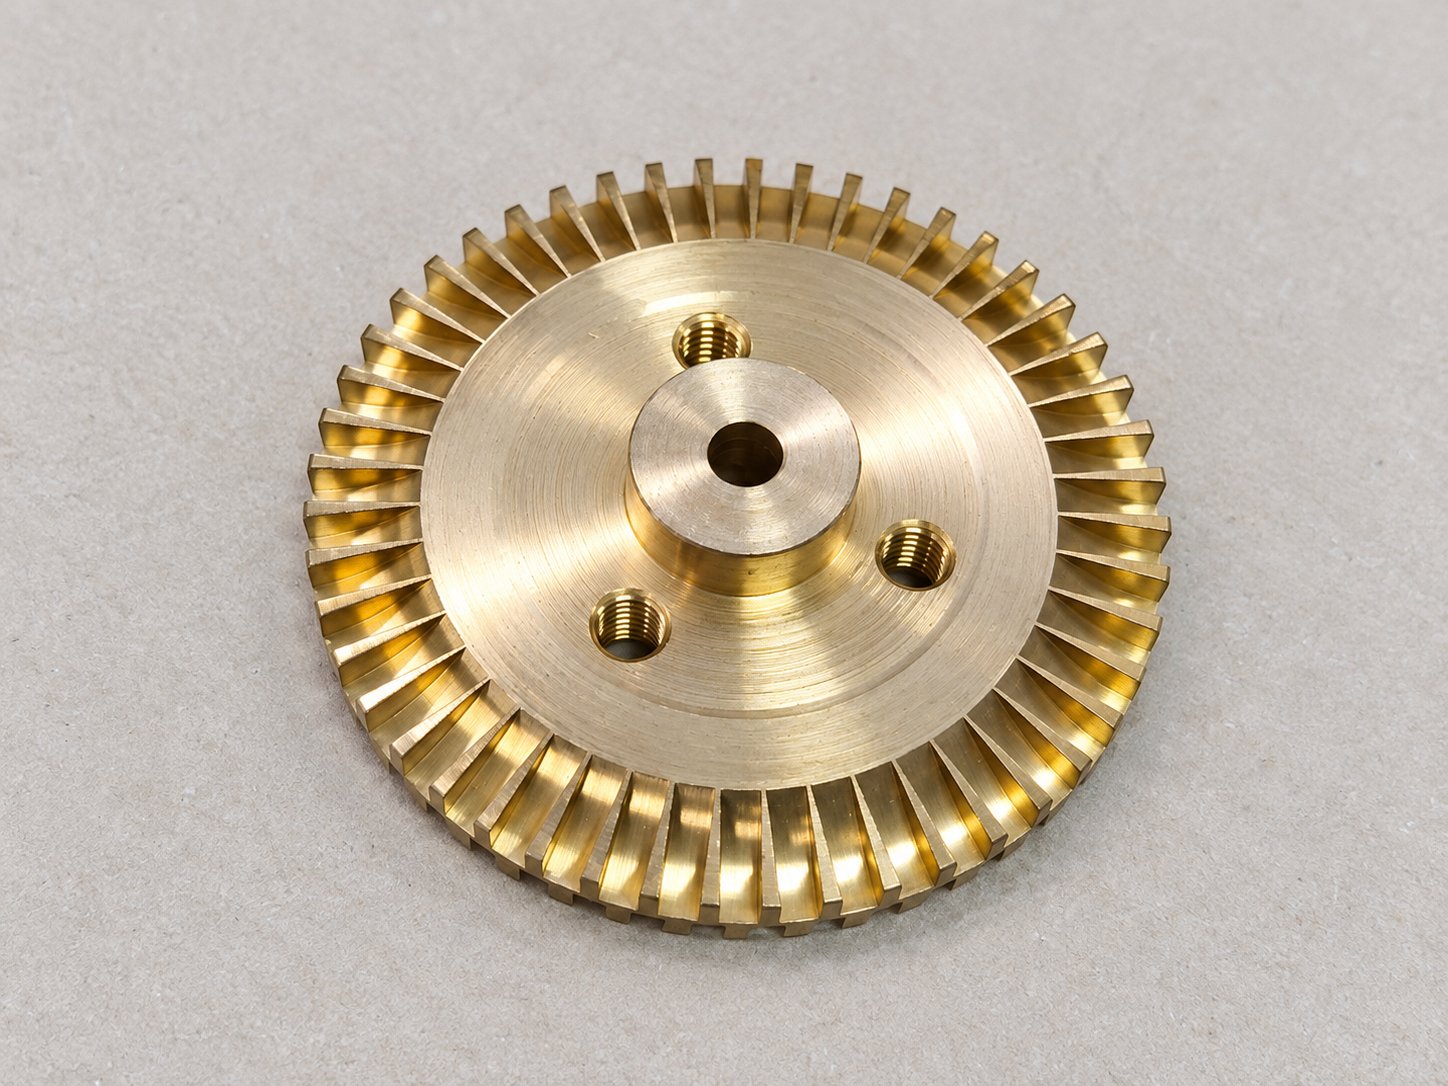
Brass pump impeller
An impeller produced in continuous lots on the Makino S33 in this factory. The vanes are milled as continuous curved surfaces on the Makino S33; the shaft bore and three tapped holes reference the same centre as the vanes to keep the part balanced in rotation.
- Machine
- Makino S33
- Material
- Brass
- Process
- 3D vane milling · boring · drilling and tapping
- Type
- Continuous production lots
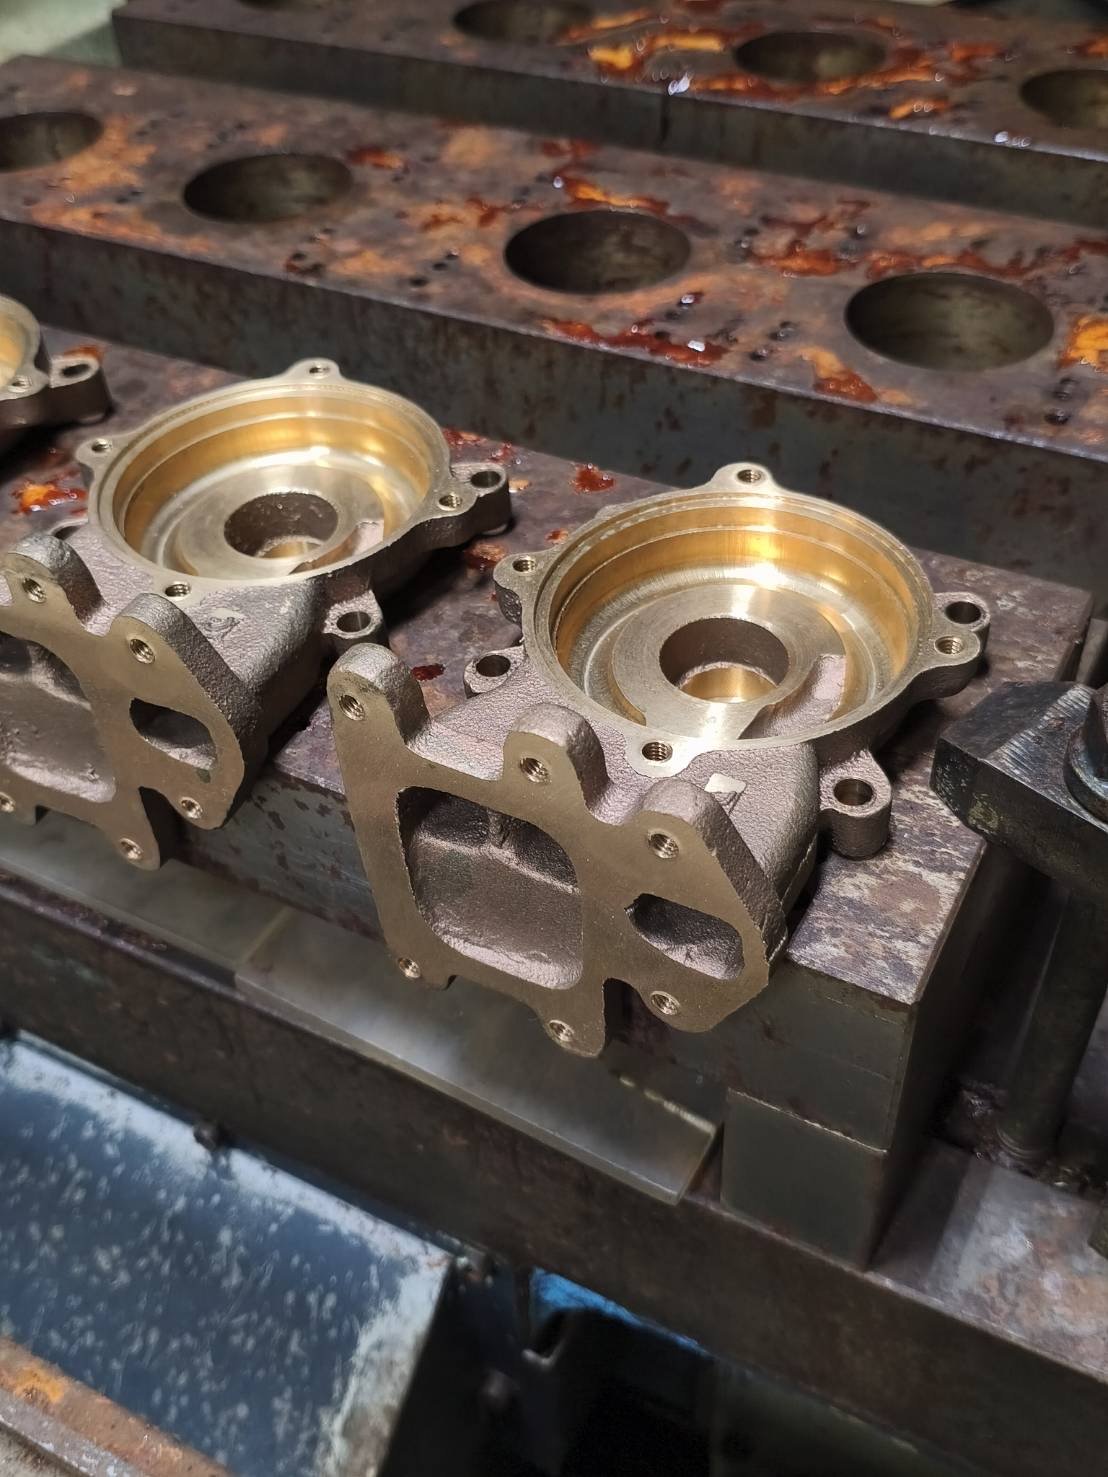
Cast pump impeller covers
Castings that need a flat mating face, a bored assembly recess and drilled-and-tapped fixing holes. Run in lots on the S33 on a multi-part fixture, all referencing the same datum, with first-article inspection before the lot and in-process checks at the critical features.
- Machine
- Makino S33
- Material
- Casting (customer-supplied welcome)
- Process
- Face milling · boring · drilling · tapping
- Type
- Lots, multi-part fixture
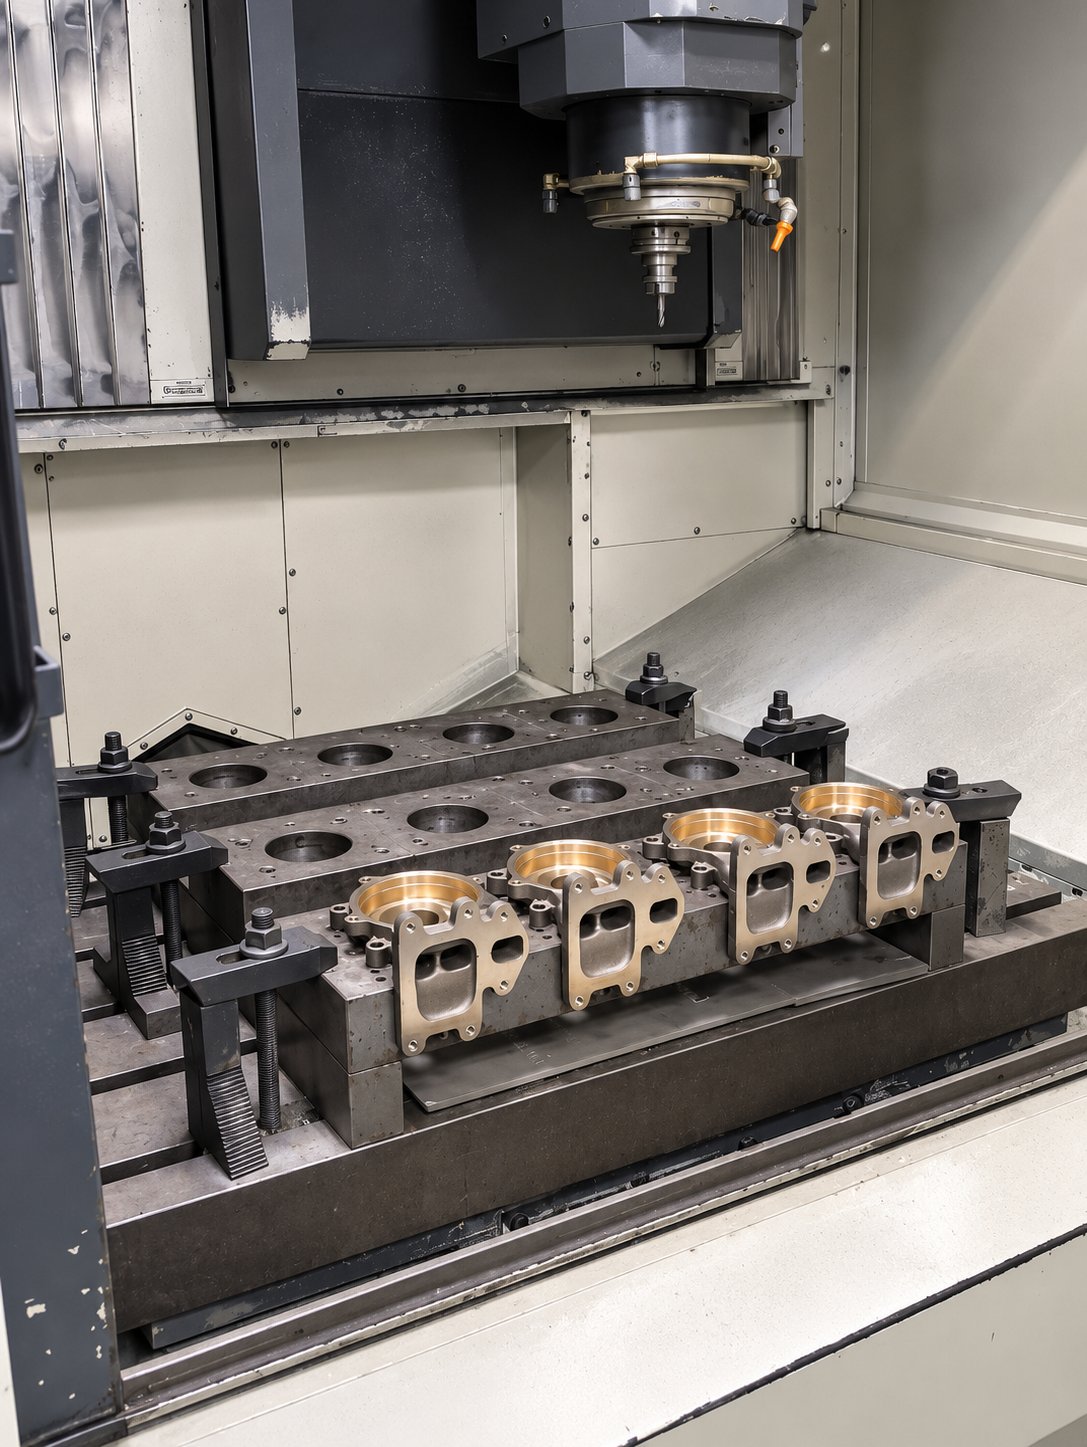
A production lot on the Makino S33
Fixtures designed and built in-house make set-up fast and put every part in the same position, cycle after cycle. This is how we keep unit price and quality stable over continuous lots — the same discipline as the group’s production lines.
- Machine
- Makino S33 · 13,000 rpm · 20-tool ATC
- Key point
- Multi-part fixtures, repeatable set-up
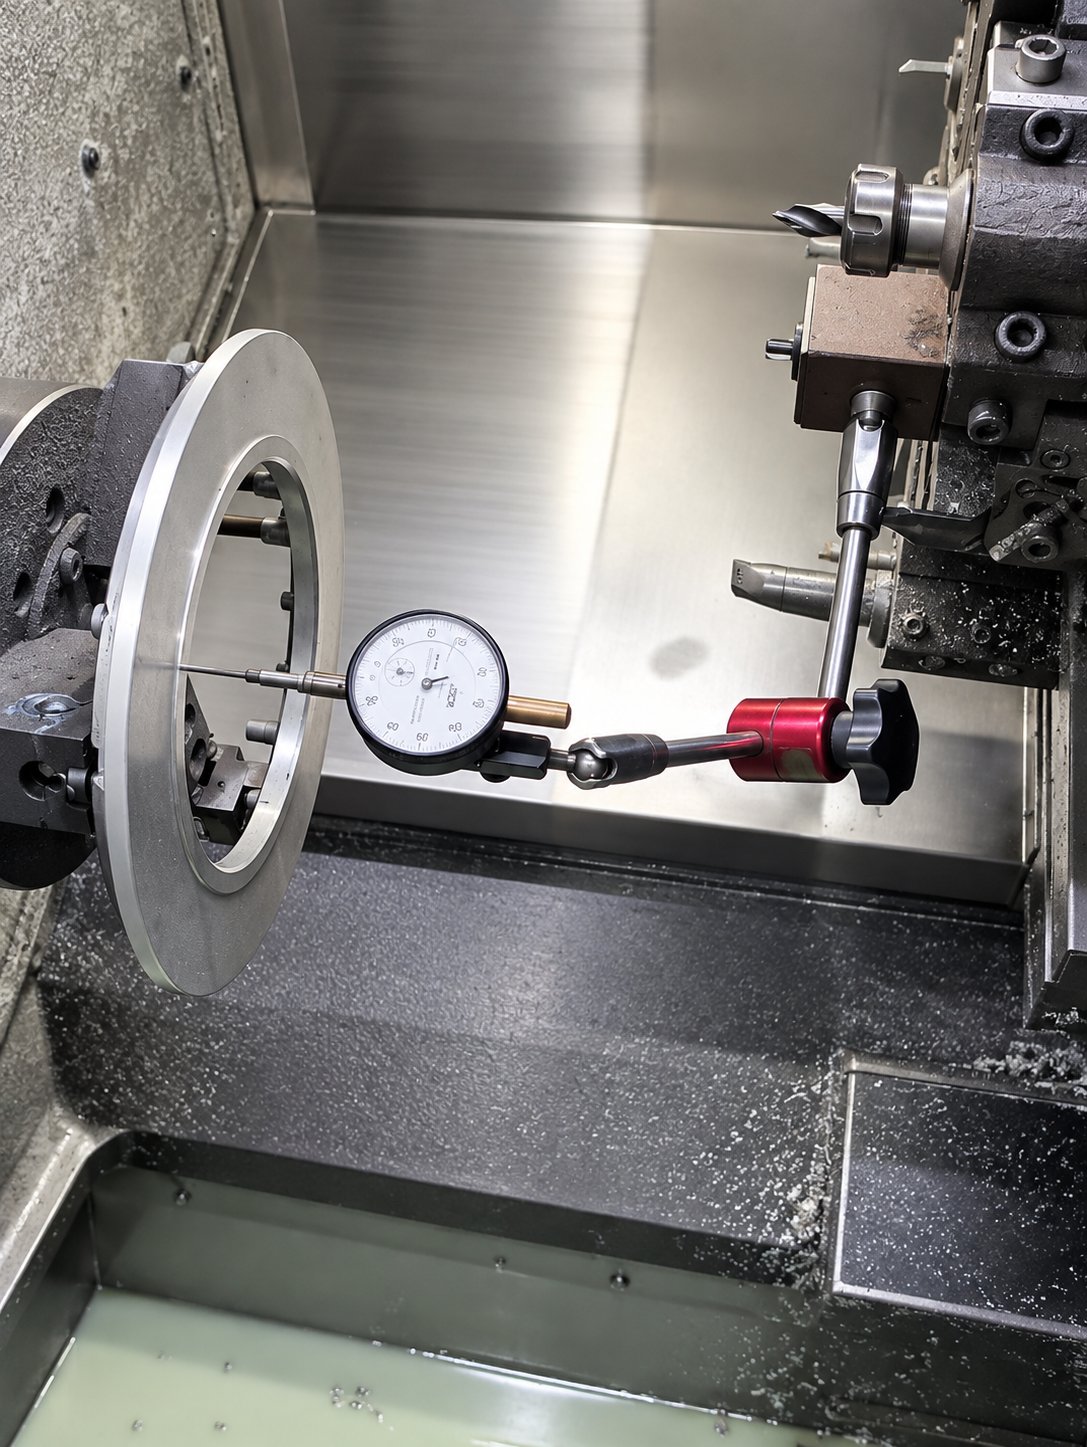
Electric stove face, turned
A face ring where flatness and runout matter because it must sit flush against the mating part. Before every lot the operator sets the part up and checks runout with a dial indicator, then faces, turns the rim and bores in one clamping.
- Machine
- Mori Seiki CNC lathe
- Process
- Facing · rim turning · boring
- Inspection
- Dial-indicator runout check · first article
Work that fits our machines and our team
Impellers and pump components
Brass impellers, impeller covers, pump housings, flanges — for pump, valve and fluid-machinery makers.
Castings that need finish machining
Face milling, boring, drilling and tapping on your castings, in lots on fixtures — for foundries and machinery builders.
Appliance and machine parts
Turned rings, flanges, bushings and shafts, turn-mill parts in one setup, jigs and fixtures, and repair work — for appliance makers, machinery builders and plants that need an outsourced machine shop.
From drawing to delivery
An engineer reviews the drawing, plans the process, tolerances and measurement method, and replies with the quote and any production notes.
Lots get a multi-part fixture; single parts get a milling/turning sequence that finishes under one roof.
The first part is measured against the full drawing with calibrated gauges; the lot runs only after it passes.
Critical features are checked during the lot and recorded per lot. A measurement report is attached on request; CMM reports come from an external laboratory.
Send us your drawing
A PDF is enough — add material, quantity and delivery date. An engineer reviews it before we quote.